Why Does Electrostatic Powder Coating Peel Off Galvanized Steel?
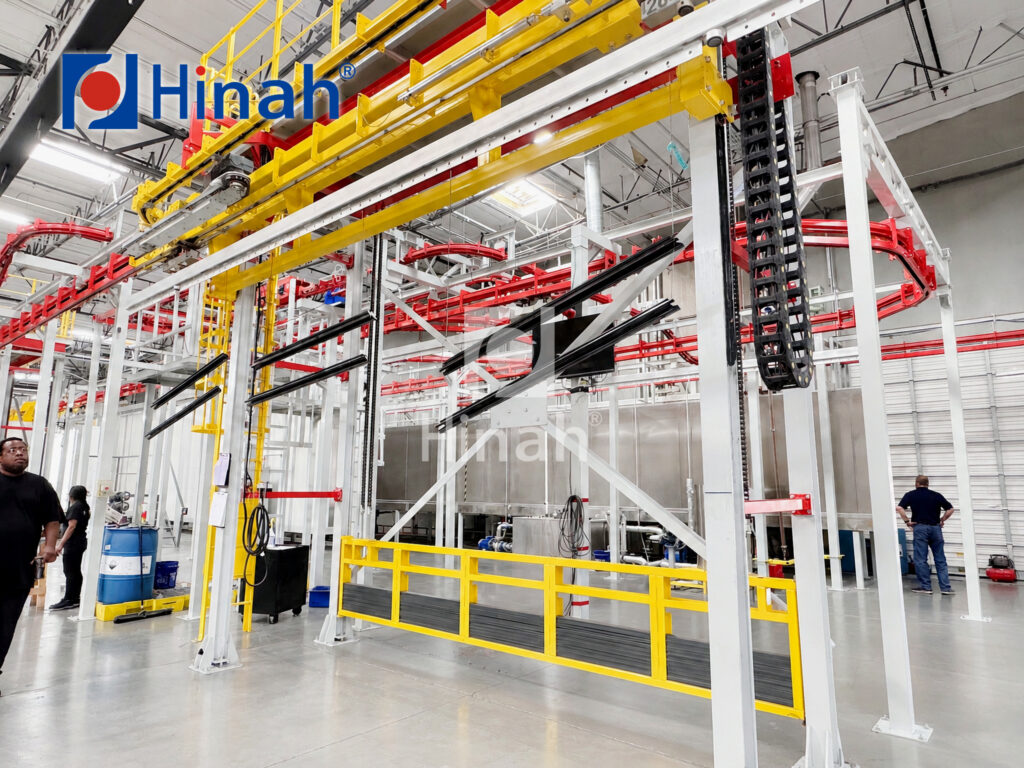
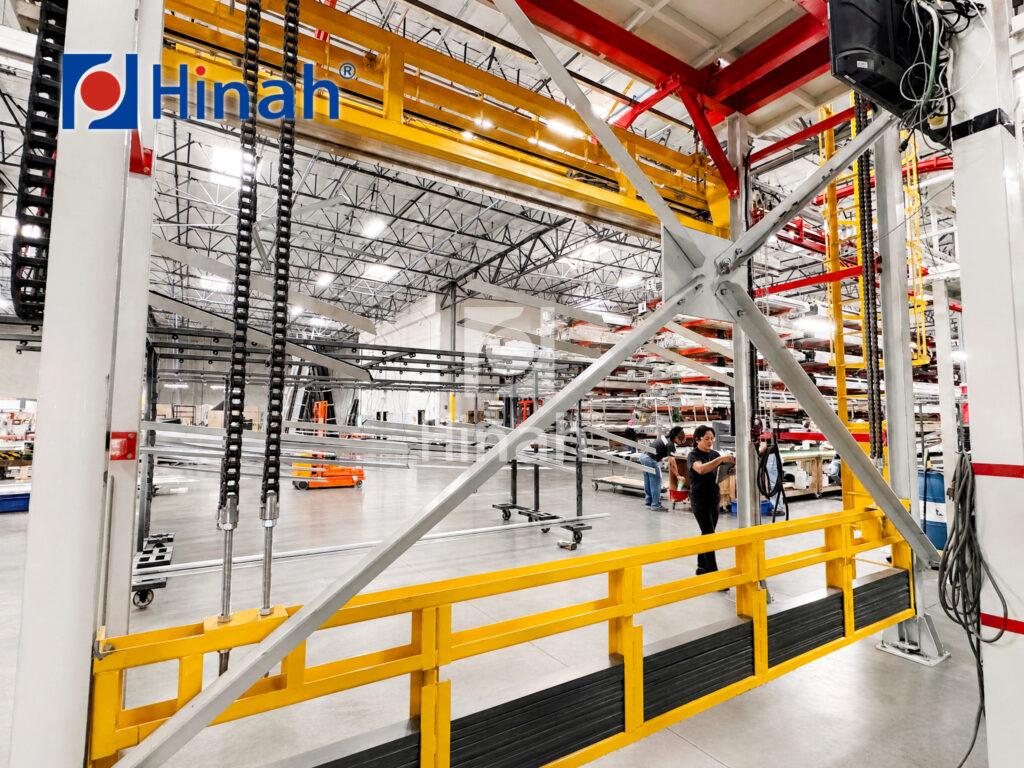
Electrostatic powder coating peels off galvanized steel at the interface, not in the film. Three things drive it: a passivation layer the galvanizer left behind, a pretreatment that suits cold-rolled steel but not zinc, and gas trapped inside the zinc layer that escapes during cure. Change the powder and nothing improves, because the powder never caused the failure. On an automatic powder coating line, the washer and the oven decide the result.
What Makes Galvanized Steel a Hard Substrate?
A hot-dip coating is not paint on steel. ASTM A123 and ISO 1461 set the zinc mass by section thickness, and that zinc stays chemically active long after the part leaves the kettle.
Zinc reacts with alkaline cleaners, with acids, and with humid air. Most galvanizers apply a chromate or chromium-free passivation to stop white rust in transit. That film does its job on the truck, then blocks adhesion in the booth.
The surface also arrives smooth. Cold-rolled steel offers a profile that grips a film. Zinc offers almost none, so the bond has to come from chemistry rather than mechanical keying. That is why electrostatic powder coating on galvanized work depends on the washer and the phosphate stage more than on the gun.
How Does Electrostatic Powder Coating Bond to Zinc?
Two things hold a film on zinc: a conversion coating and a clean interface.
Iron phosphate, the workhorse for steel, builds a thin, partly crystalline layer that suits cold-rolled sheet. It performs poorly on zinc. Zinc phosphate grows the right crystal structure on a galvanized face, and coating guides such as the Powder Coating Institute handbook steer galvanized work toward zinc phosphating. The stage count of the washer decides which chemistry a line can run, and that choice is worth settling before the booth is built.
Coating weight matters as much as chemistry. A heavy phosphate layer fails inside itself, so the crystal shears before the bond to zinc does. Most lines run a light coat of 1.5–2 g/m².
Cleaner choice decides the rest. Caustic cleaners attack zinc and leave zinc hydroxide behind, and that hydroxide later turns into a weak boundary under the film. A 3-stage and 5-stage pretreatment run with the wrong chemistry still fails, even when every bath sits in range.
Why Do Pinholes Appear After the Oven?
Hot-dip galvanizing leaves a porous zinc layer that traps air, moisture and flux residue. Heat drives those gases out. They pass through the powder film while it still flows, and the film sets with craters, pinholes or small blisters.
A pre-bake solves most of it. Run the part at 200 °C for 20 minutes, let it cool, then coat. The gas leaves before the powder arrives instead of during cure.
Powder choice helps too. Outgassing-resistant grades tolerate a rougher substrate, and a thinner film shortens the path the gas must travel.
Which Failure Are You Actually Looking At?
Five patterns cover most galvanized complaints about electrostatic powder coating.
– Pinholes and craters across the face: trapped gas from the zinc layer. Check the pre-bake step and film thickness.
– Film lifts in sheets after humid storage: alkaline residue or a heavy phosphate layer. Check final rinse conductivity and coating weight.
– Peel at cut edges and drilled holes: thin coverage on sharp geometry. Check gun paths and edge film build.
– White powder under the film: white rust nobody removed. Check incoming inspection and storage.
– Blisters at one rack position: poor ground contact and uneven cure. Check hook condition and the oven profile.
How Do You Specify Electrostatic Powder Coating for Galvanized Parts?
Write the sequence, not the wish list:
– Clean with a neutral or mild alkaline cleaner, and hold bath pH in range.
– Rinse twice, and keep the final rinse under 30 µS/cm.
– Apply a light zinc phosphate.
– Dry off before the booth.
– Pre-bake at 200 °C whenever cure runs above 180 °C.
– Cure to the powder datasheet, measured on the metal, not in the air.
Prove it with ASTM D3359 tape, ASTM D4541 pull-off and ASTM B117 or ISO 9227 salt spray. ISO 12944-5 links each durability class to a salt-spray target, so a C4 application sets the hours instead of a guess.
What Still Goes Wrong on a Running Line?
Three habits undo a good electrostatic powder coating specification. Operators skip the pre-bake when the schedule slips. Parts sit outside and collect white rust before they reach the washer. And cure drifts upward, because a faster line pushes the oven set point until the film embrittles.
Keep galvanized stock indoors, coat it within a few days, and log metal temperature every shift. None of that adds cost.
In short: electrostatic powder coating fails on galvanized steel because zinc is a reactive, smooth and gassy substrate, and a steel-oriented process ignores all three. Fix the passivation removal, the phosphate chemistry and the trapped gas, and the same powder that peeled last month will hold for years. Send a part drawing and a service class, and we will match the pretreatment and cure schedule to it.