If the Inside of the Part Stays Bare, Check Throw Power
Bare steel inside a coated part means the field stopped short of that surface. Throw power describes how far an electric field drives paint into a cavity. It decides whether a boxed section, a welded seam or a tube end ever gets covered. Voltage on the outer skin tells you nothing about that depth.
What Does a Bare Inside Actually Mean?
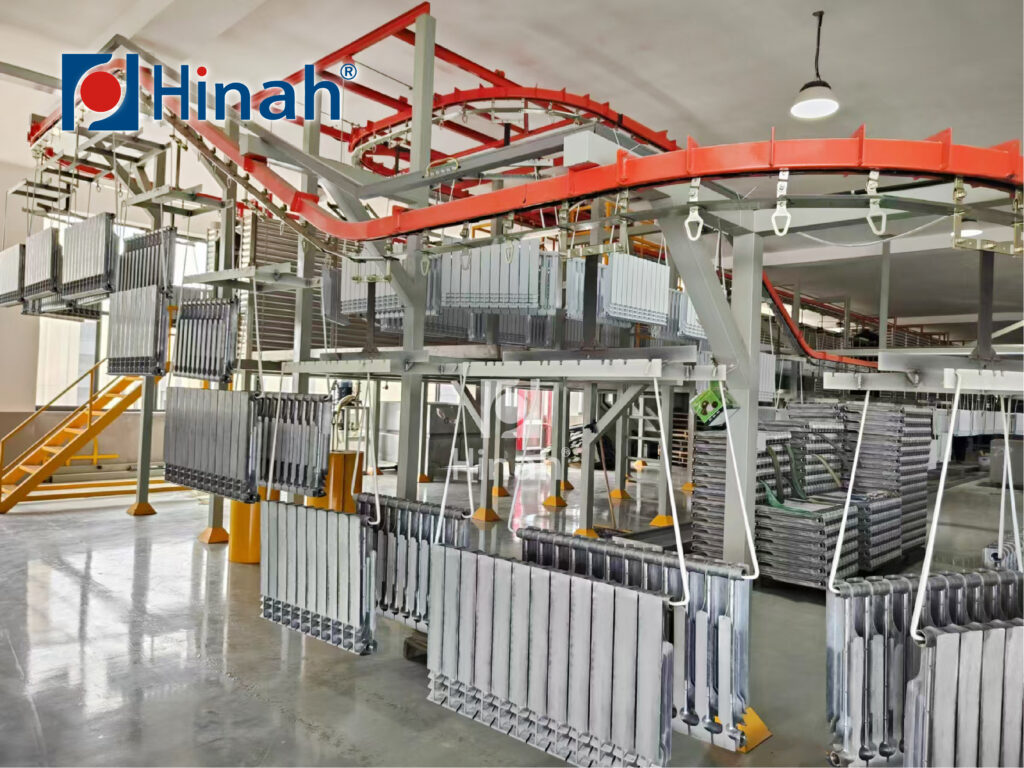
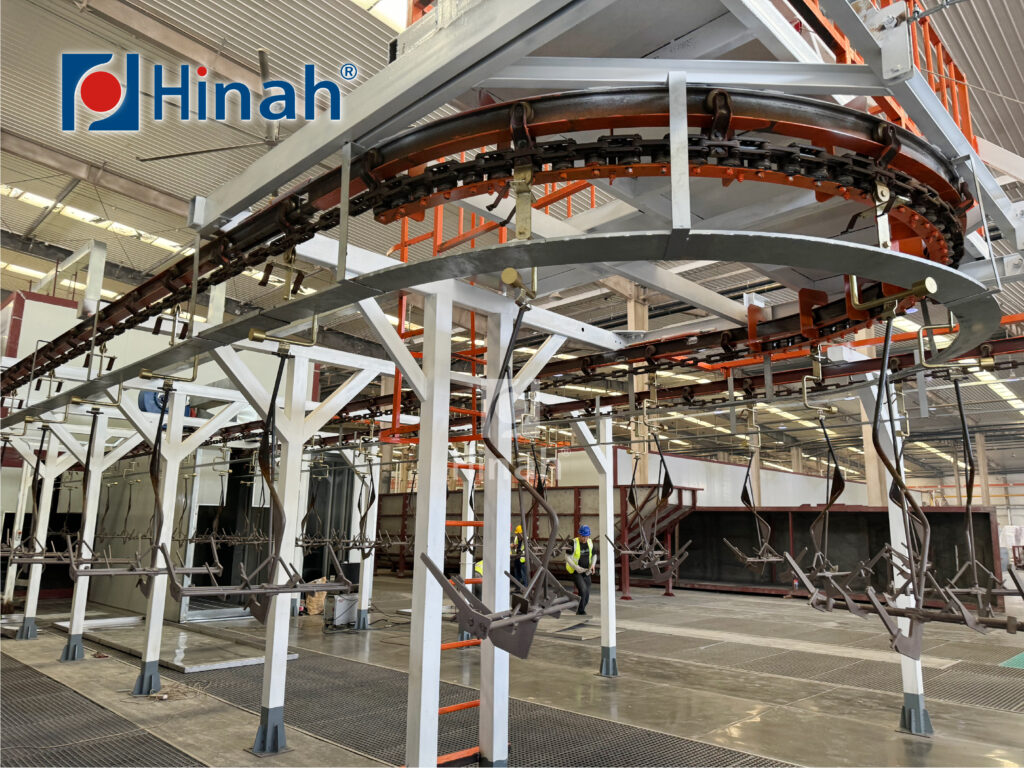
Look at where the steel shows before you touch the rectifier. A completely bare interior with a normal exterior film points to a field that cannot reach — the classic throw power symptom. A patchy interior, bright at the opening and bare at the back, points to geometry: the opening is too small for the depth behind it. A thin but present interior film that later fails salt spray points to the pretreatment tank or the cure oven instead.
The three take different fixes, and the expensive mistake is treating a geometry problem with voltage. Cut one cured part open and measure both surfaces. A magnetic gauge to ISO 2178 on steel, or an eddy-current gauge to ISO 2360 on aluminium, gives you the two numbers. Their ratio is your starting point, and it is the only figure that says whether the field reaches or falls short.
Sealed cavities and double-wall sections deserve a separate look. No bath chemistry and no voltage setting reaches a volume with no opening. If the drawing shows a closed box, the answer sits on the drawing, not on the line.
What Sets Throw Power on an E-Coating Line?
Four things decide it, and only one of them sits on the control panel.
Throw power belongs to the field the part sits in on an e-coating line, not to the paint in the tank. Bath conductivity and solids set how current spreads through that field. Part geometry sets how much of the current can turn the corner. A deep pocket behind a narrow opening starves; a shallow pocket behind a wide one fills. Electrode distance and racking set the field shape around the part. The face turned toward the anode coats first and heaviest, while surfaces in the part’s own shadow coat last.
Voltage supplies the driving force, and it acts on all four at once. That is why turning it up rarely fixes a thin interior; the outside takes the extra current long before the inside does. Deposition is self-limiting as well. As film builds, resistance rises and current falls, so a surface that starts starved tends to stay starved for the rest of the cycle.
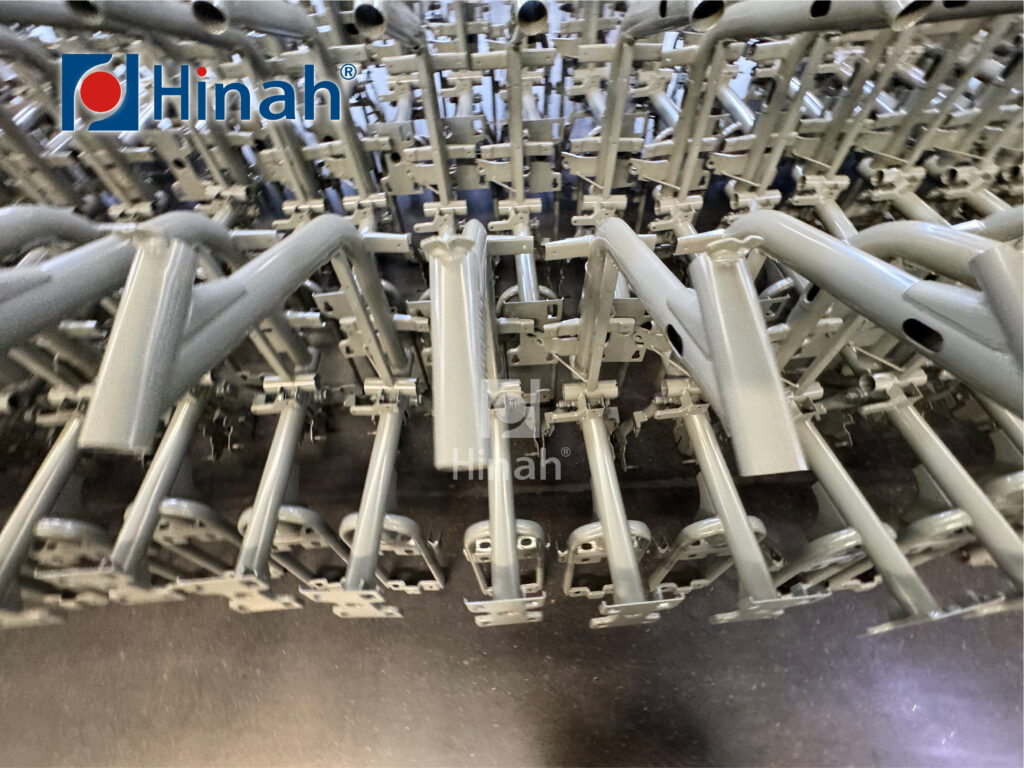
Why More Voltage Makes the Outside Worse
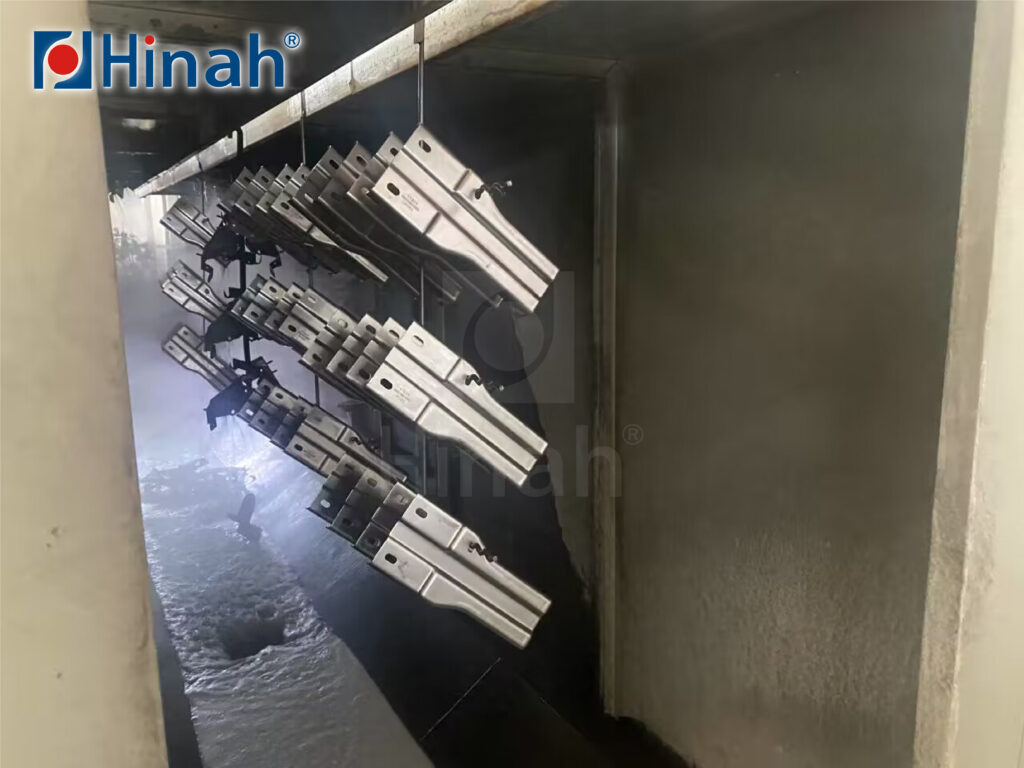
Raising voltage thickens every surface the field already reaches, and the outside reaches first. The exterior film grows heavier. Cratering and rupture risk rise at edges, paint use climbs, and the interior still misses spec. The limit inside is the current path, not the driving force.
More voltage does not buy throw power into a shadowed cavity, because the path starves before the force matters.
Thick sections add a second penalty. Extra film means more mass to heat, a longer oven dwell, and a wider gap between thin and thick parts sharing one load. Overbake on the thin sections follows. Treat voltage as the last dial to turn, not the first. When the interior ratio is short while the exterior already sits at spec, the line has a field-shape problem. Field shape comes from racking, part design and bath condition.
What to Check, in Order
Racking comes first because it costs nothing. Rotate the part so the cavity faces the anode, run the same part again, and compare the interior film.
Ground path comes second. A coated hook behaves like an insulator, and it starves whichever surfaces sit furthest from the electrode. Confirm metal-to-metal contact at the hanger and along the carrier.
Bath condition comes third: solids, conductivity, temperature, solvent balance. All four drift slowly, and none of them shows on the part until the interior fails.
Part design comes fourth, and it is usually the real fix. A drain hole at the low point, a vent hole at the high point, a shorter blind depth — each one changes how much field reaches inside. Rectifier settings come last.
Recheck the inside-to-outside ratio after every move, on the same part, from the same rack position. Each change alters the throw power you measure, and a single reading taken after five changes tells you nothing about which one worked.
If the interior still misses spec after all four, the part may not suit e-coat at all. A design change or a different process for that surface is the honest answer at that point. No voltage setting repairs a cavity the field cannot enter.
Bare interiors are a reach problem, and throw power is how you measure the reach. Measure inside against outside on one cut part, and let the ratio tell you whether to move the rack, the bath or the drawing.